Welcome to Moore Automation Limited
How to reduce downtime and extend the useful service life of an established machinery protection system.
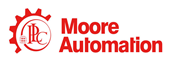
The Bently Nevada 3500 Machinery Protection System is widely used to protect turbines, compressors, generators, motors, pumps and other critical rotating machinery. More than 85,000 systems have been installed worldwide, providing continuous monitoring and automatic protection against damaging machine conditions. When connected to System 1 software, the platform can also support proactive maintenance with continuous condition information.
Effective maintenance begins with a record that reflects the system currently installed, not only the original project drawings. Years of replacement, expansion and configuration changes can leave the actual rack arrangement different from early documentation.
The rack configuration is part of the machinery protection function. Before replacing or reconfiguring a module, retain a controlled backup identified by machine, rack and revision date. Supporting records should cover channel settings, alarm values, relay logic and communication parameters.
After maintenance, compare the restored configuration with the approved baseline. A replacement module should never be assumed to contain the correct machine-specific settings.
A monitor channel depends on more than the card installed in the rack. A typical proximity measurement chain may include the probe, extension cable, Proximitor sensor, field wiring, termination points and the corresponding 3500 monitor channel.
When a signal becomes unstable or a channel enters Not OK condition, inspect connectors, cable insulation, probe gap, shielding, grounding, junction boxes, transducer output and channel configuration. This complete-loop approach helps prevent unnecessary module replacement when the actual problem is located elsewhere.
Routine inspection should include rack, module and channel status. Record repeated Not OK events, bypassed channels, communication interruptions, power-supply conditions and unexpected measurement changes together with the operating state of the machine.
System 1 integration can add trends and event information to the maintenance process. This allows teams to evaluate developing machinery behavior before it becomes a forced shutdown rather than responding only after an alarm or hardware failure.
Maintenance work should minimize the period during which a monitoring channel or shutdown function is unavailable. The work scope must be coordinated with plant procedures and the protection requirements of the machine.
A stored spare reduces downtime only when it matches the installed application. Check the complete product number, channel capability, hardware revision, firmware requirements, configuration requirements and rack compatibility before the part is placed in emergency stock.
Spare quantities should reflect the actual rack population and machine criticality. Bently Nevada 3500 monitoring cards are not backward compatible with the earlier 3300 monitoring platform, so the two system families must be identified and managed separately.
An OK indication alone does not complete a module replacement. Confirm module recognition, channel configuration, transducer status, expected measurement values, Alert and Danger functions, relay logic, communication and removal of every temporary bypass.
An upgrade should be based on operational needs rather than age alone. Assessment becomes appropriate when repeated faults affect protection availability, compatible hardware is difficult to manage, new machinery changes the monitoring scope, or newer integration and diagnostic functions are required.
A phased migration can be coordinated with scheduled machinery outages. Accurate rack documentation and configuration records also provide the foundation for engineering a controlled transition to Orbit 60 or another suitable monitoring platform.
| 330130-080-02-05 | 330104-00-07-50-02-00 | 330180-91-CN |
| 330180-51-00 | 3RW4075-6BB44 | 51305907-175 |
| 3TK2825-1AL20 | 3TK2828-1AL20 | A145-30-11 |
| 5506 | TBUX297319 | 6ES7412-3HJ14-0AB0 |
| B13000 F1 | MTL4575 | GSH204 AC-C63/0.03 |
| AF400-30-11 | 51303940-250 | CC-TCNT01 |
| M102-M | MD21 | CC-PAOH01 |
| CC-PAIM01 | CC-PCF901 | RDT300 |
| ALR 20/A EX | MTL5081 | MTL4073 |
| MTL5544D | CC-PDOB01 | 5405-24 |
| 5304 | 5541 | 5103 |
| TBUX297102 | MTL4015 | TBUX297248 |
| LOGIX 520SI | CC-TAIM01 | CC-PAIH01 |
| 127610-01 | 6ES7216-2BD23-0XB0 | 51198685-100 |
| TTR200 | 6ES7322-1BL00-0AA0 | CC-PCNT01 |
| WK-2 | MTL4041B | 6ES7417-4HT14-0AB0 |
| 6SL3352-1AE35-0AA1 | CC-TAOX11 | CC-TAIX11 |
| CC-TDIL01 | BS30-R-CP6X | SK3110.000 |
| 3TX7003-1CB00 | FC-SAI-1620M | FC-SDI-1624 |
| ETS1701-100-000 | CC-TAIX01 | CC-PAOX01 |
Accurate documentation, configuration backups, complete-loop inspection, compatible spares and controlled testing can help an established 3500 system remain reliable without creating unnecessary downtime. When new capabilities or changing plant requirements justify modernization, the same records provide a sound basis for a controlled migration.
Moore Automation Sales Team
Copyright © 2004–2026 www.mvme.cn. All rights reserved.
Disclaimer: Moore Automation Limited is an independent reseller and is not an authorized distributor or representative of the manufacturers featured on this website. Product names and trademarks belong to their respective owners.